PrecisionCastingSystems.
Purpose-built equipment for aerospace turbine blades, orthopedic implants, and defense castings. Three-shift production. Zero drift.

Scroll the
Line.
Seven stages. Every machine specified. Throughput, energy, and tolerance data published — no sales call required to build your capital expenditure case.
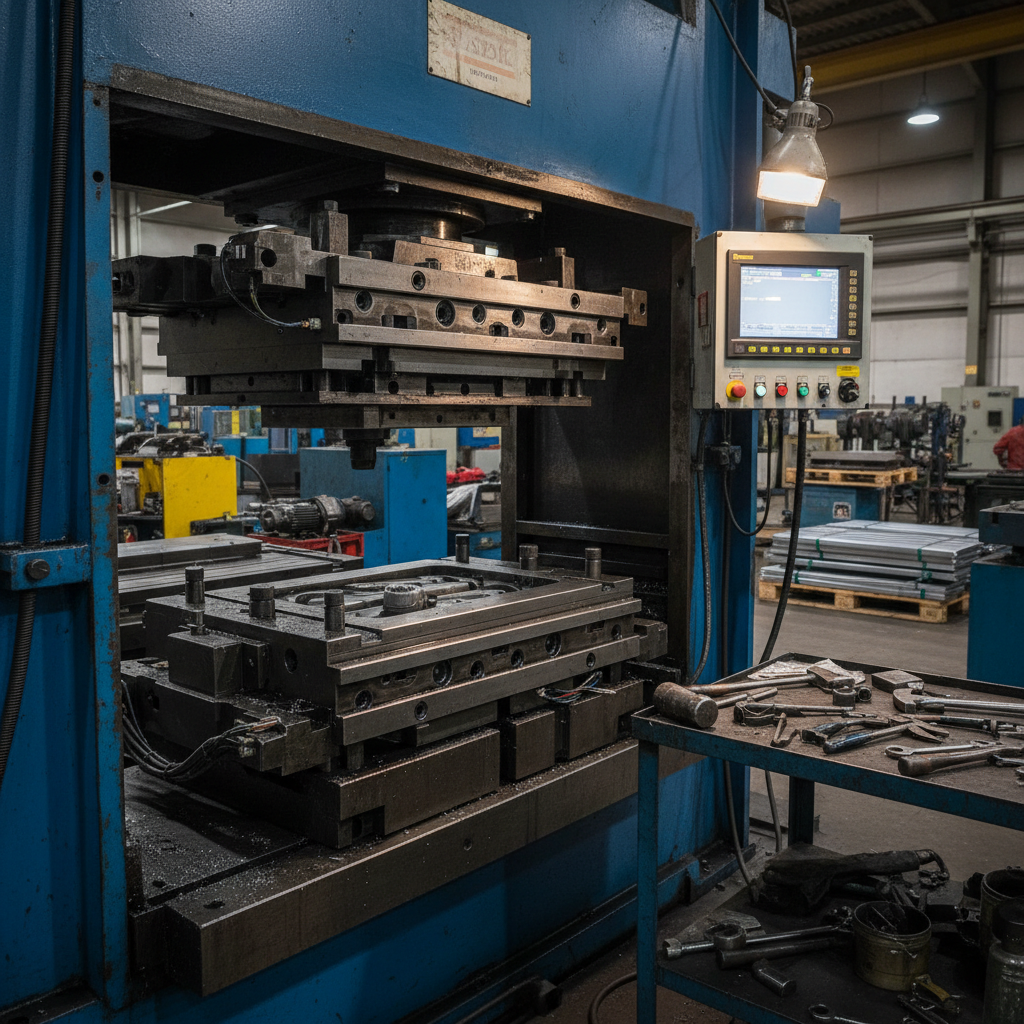
Wax Pattern Injection
FDY-WI Series Injection Press
Temperature-controlled aluminum tooling injects molten wax under 1,200 psi into precision-machined die cavities. Multi-cavity automatic tooling scales from 4 to 32 impressions per shot.
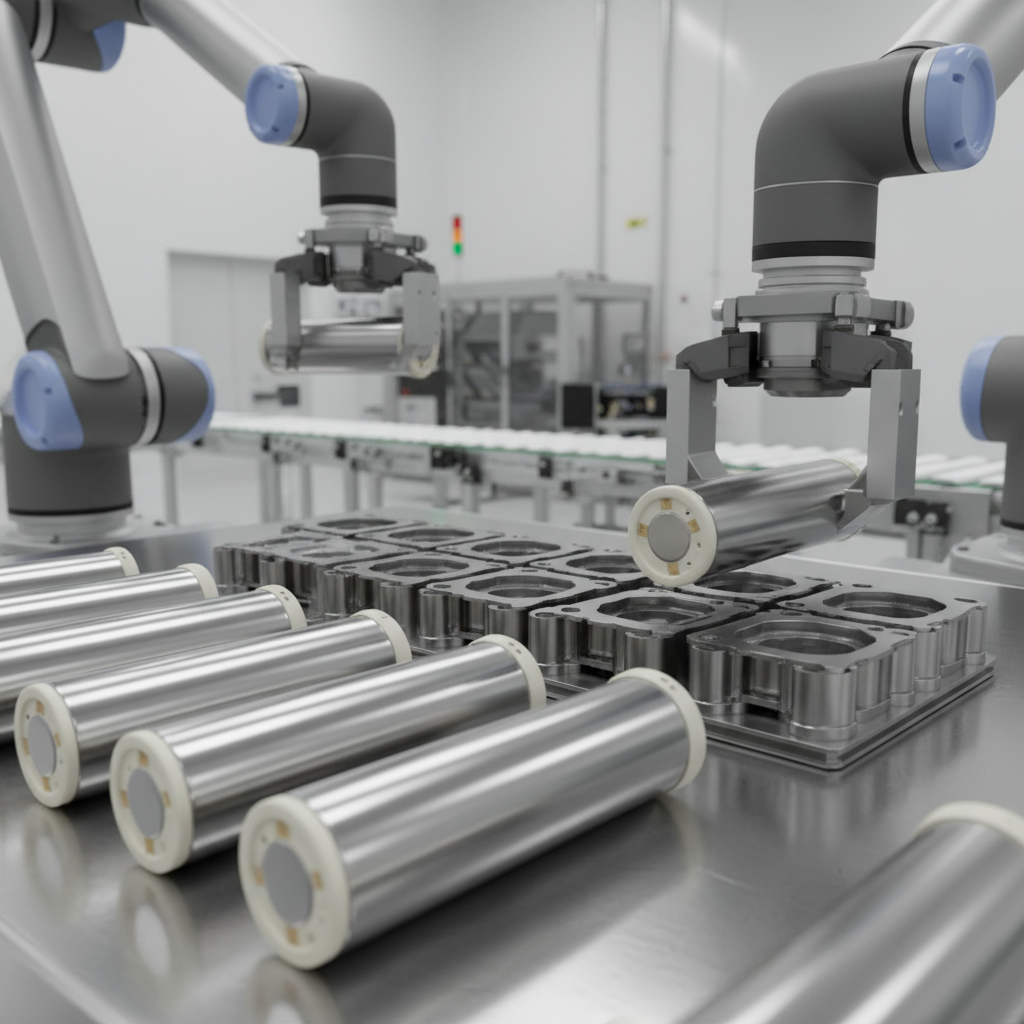
Pattern Assembly
FDY-PA Automated Assembly Cell
ABB six-axis robotic arm assembles wax patterns into cluster trees with ±0.1mm positional accuracy. Single-crystal blade assembly cells maintain orientation tolerances for directional solidification.
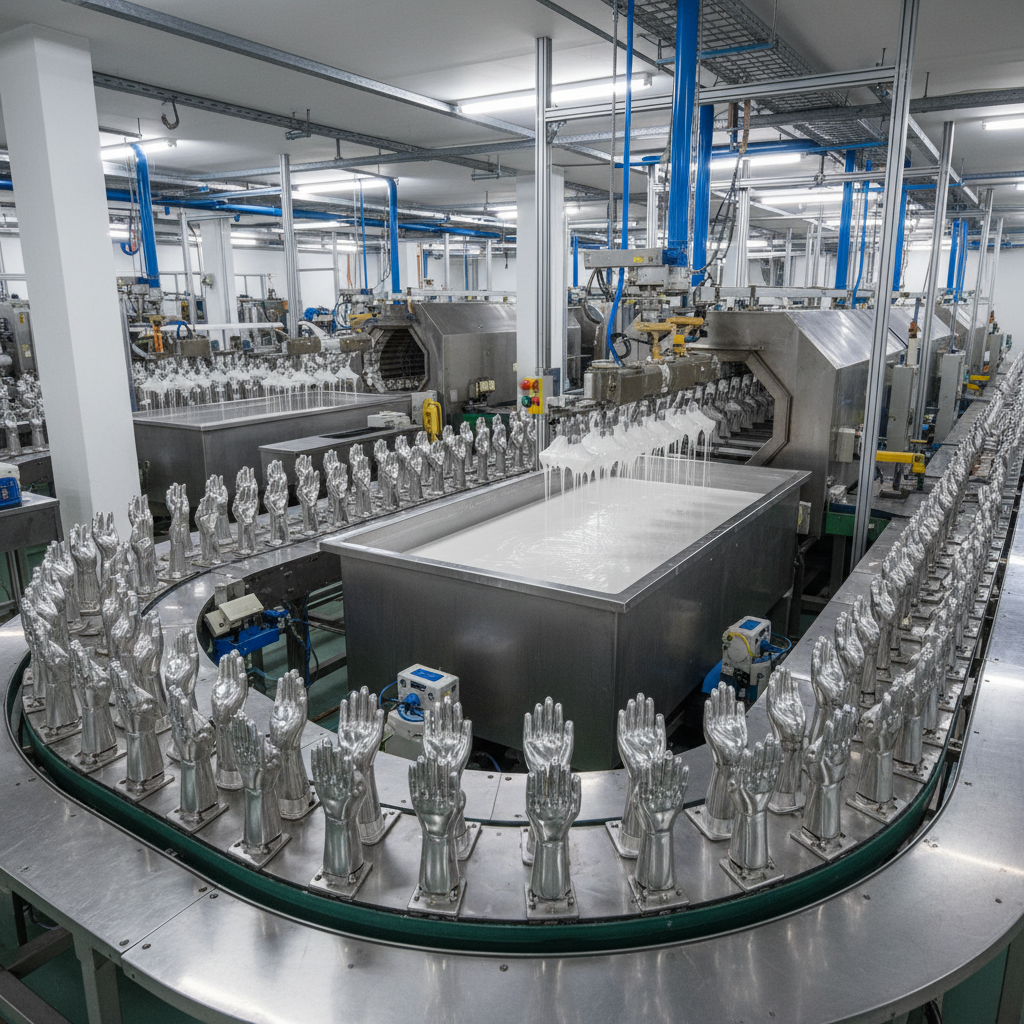
Ceramic Shell Building
FDY-SB Robotic Shell Dipper
Seven-axis dipping robot applies primary and backup ceramic slurry coats with controlled dwell times. Integrated conveyor drying system runs 24–36 hour cycles at controlled humidity and airflow.
Dewax (Autoclave)
FDY-DW High-Pressure Autoclave
Steam pressure to 90 psi at 180°C removes wax in under 8 minutes without thermal shock cracking. Closed-loop wax reclamation system recovers 94% of wax by weight for reuse.
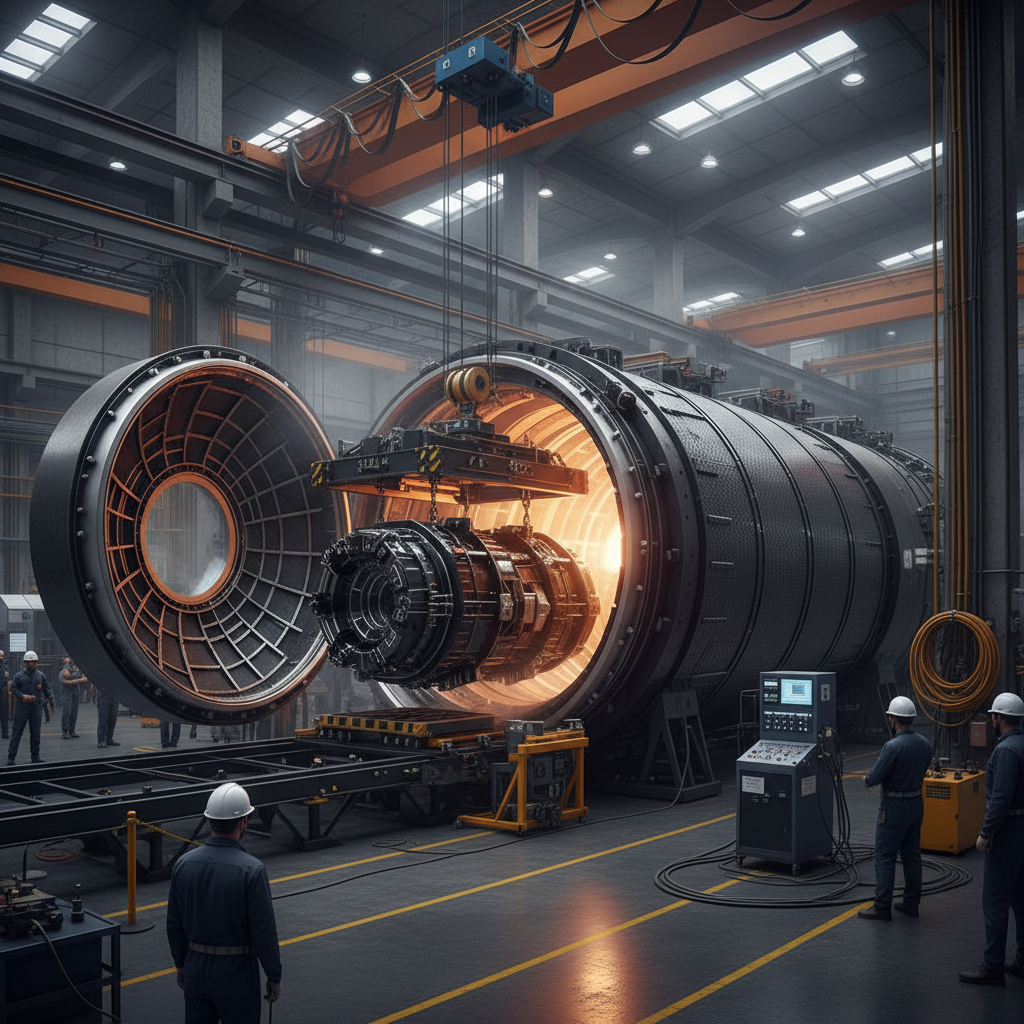
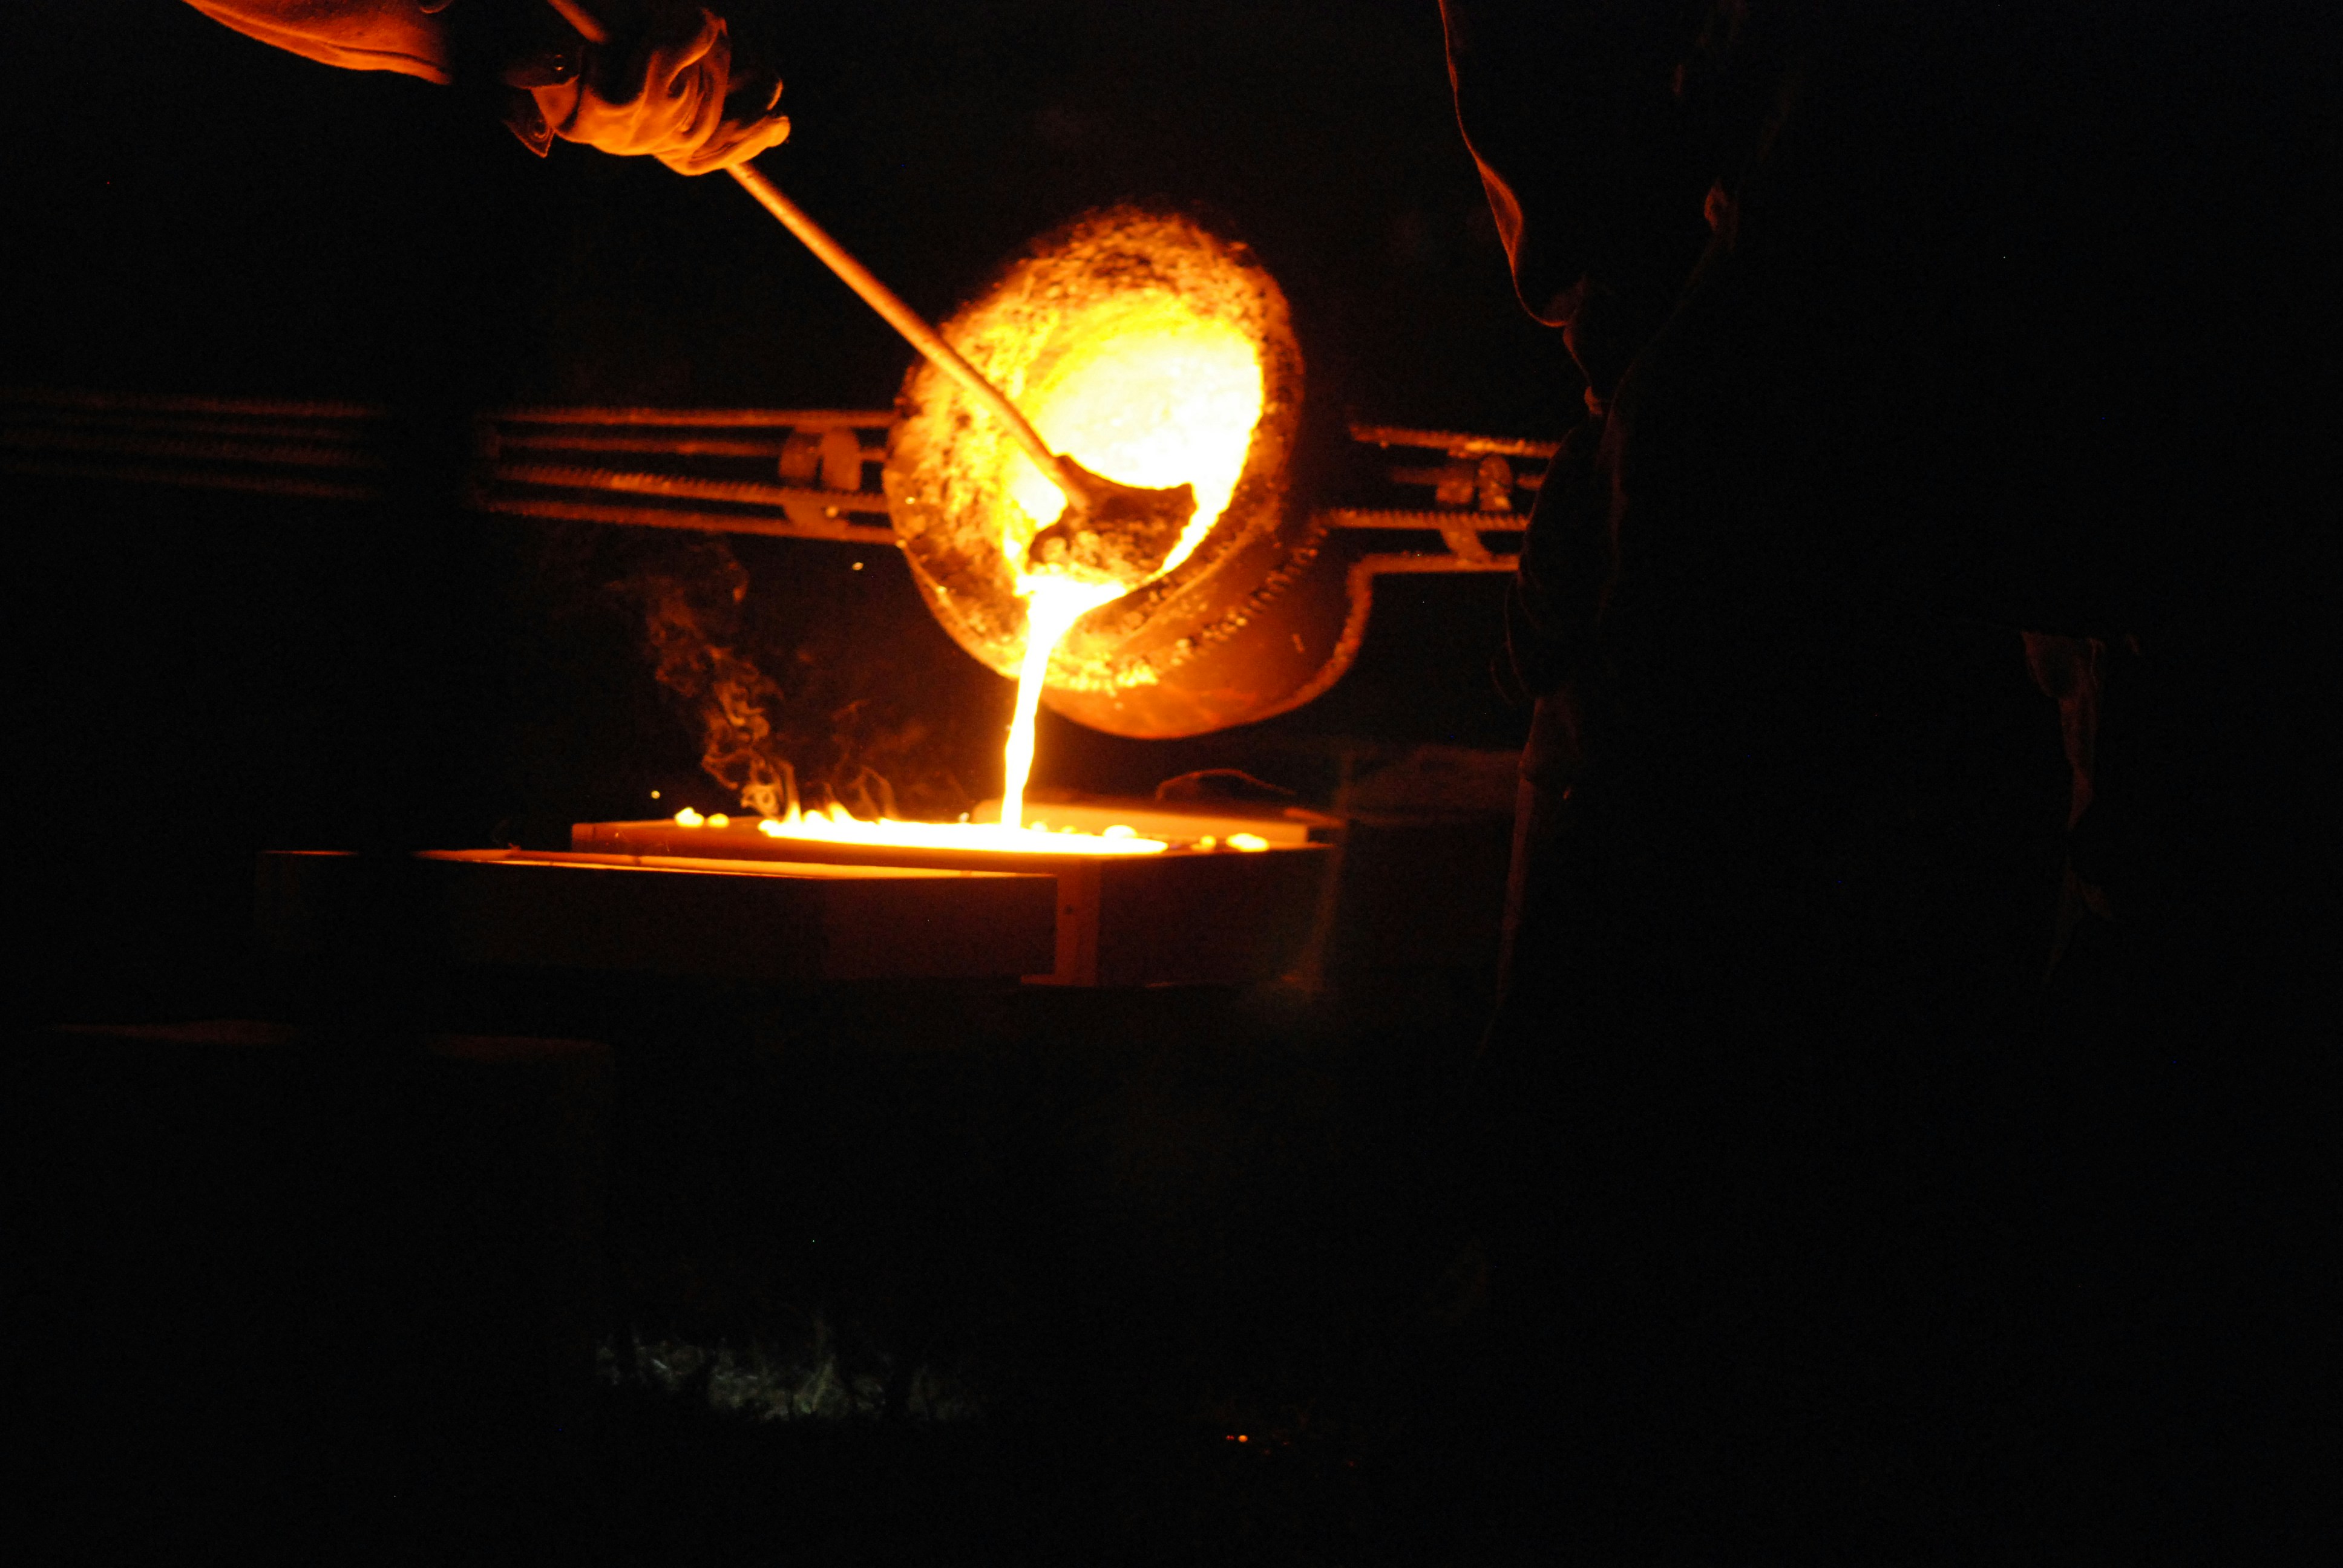
Casting Pour
FDY-VP Vacuum Induction Furnace
Preheated ceramic molds accept molten metal immediately after removal from 1,000°C cure oven. Vacuum melting option for reactive superalloys prevents oxidation and nitrogen pickup.
Knockout & Cutoff
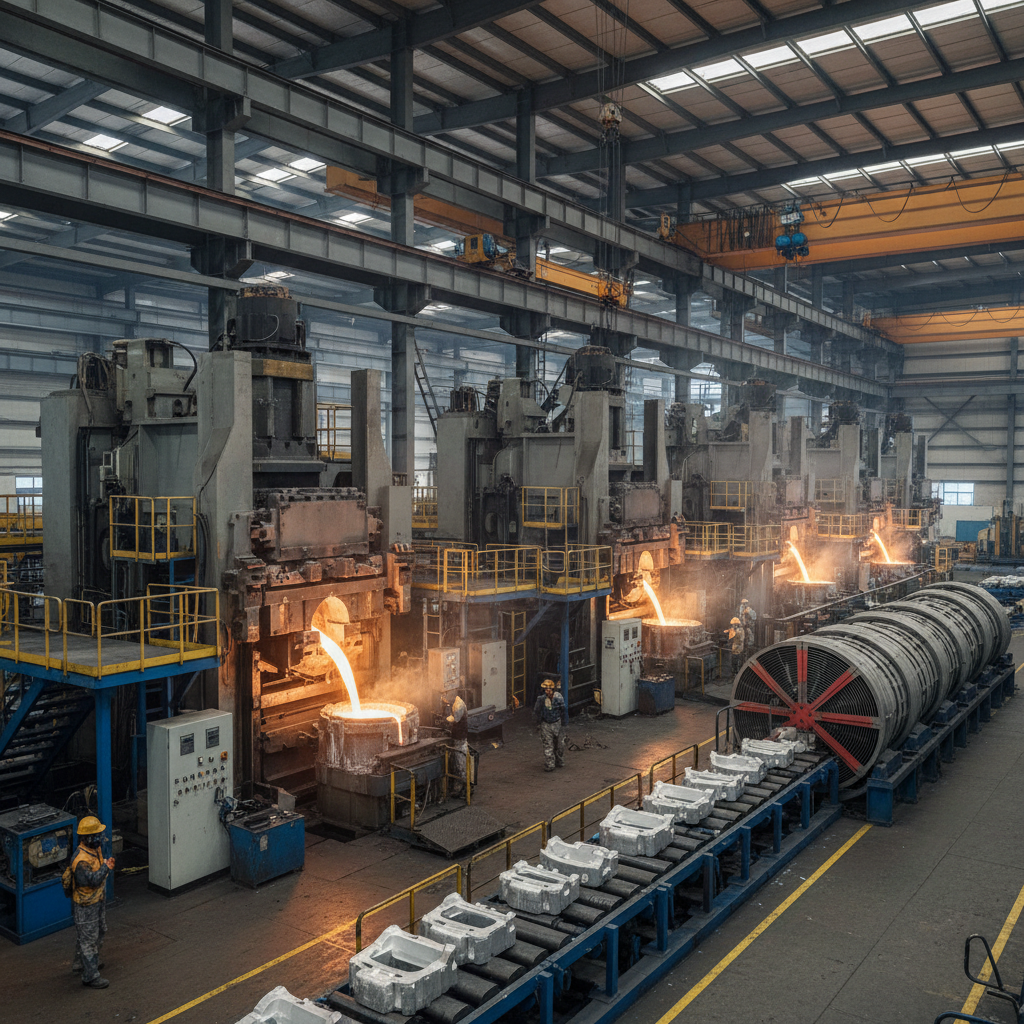
FDY-KO Vibration Knockout Station
Controlled vibration frequency shatters ceramic shell without surface damage to the casting. Abrasive cutoff saw with CNC positioning separates gates and runners to ±0.5mm.
Finishing & Inspection
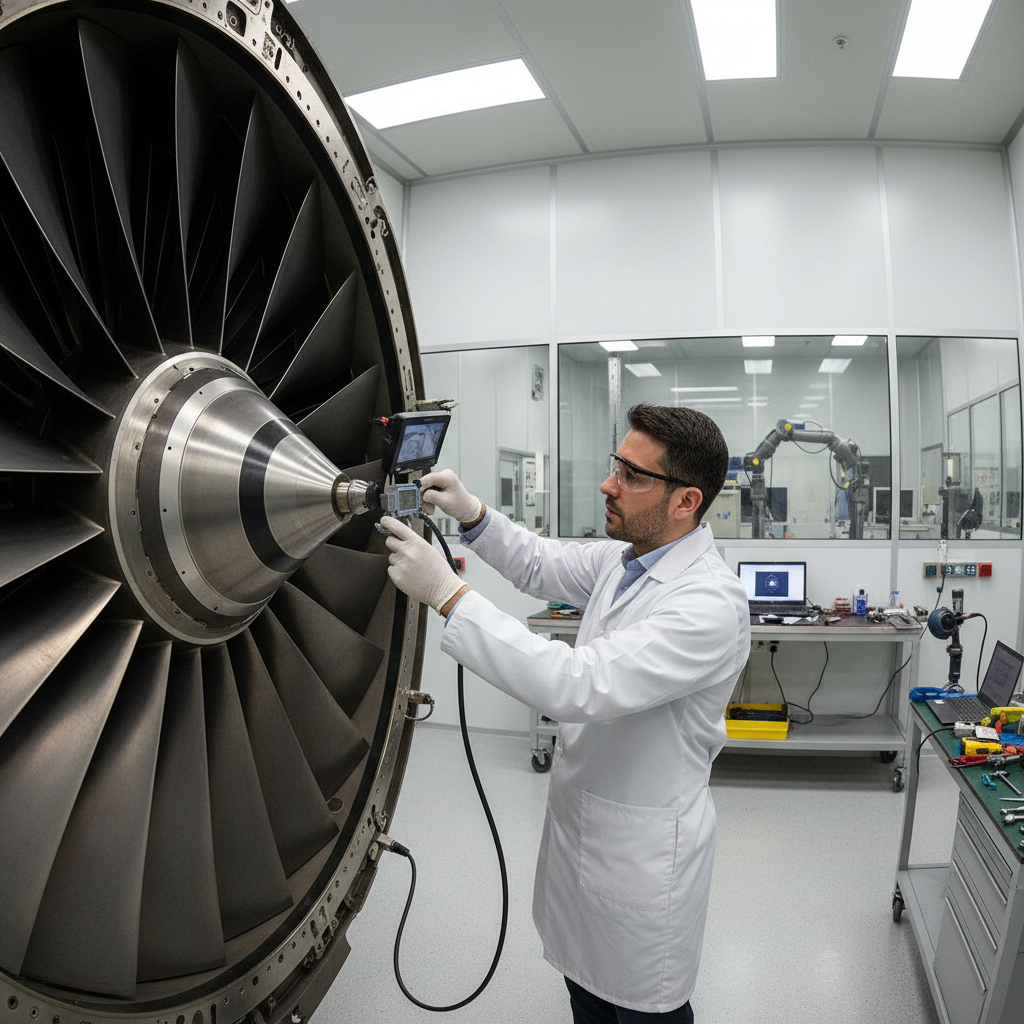
FDY-FI Automated Finishing Cell
Robotic grinding, sandblasting, and fluorescent penetrant inspection in a single automated cell. Integrated X-ray station identifies sub-surface defects to ASTM E1742 standard.
Every
Superalloy.
Foundry equipment is validated across 40+ alloy families. From nickel-base superalloys for turbine blades to biocompatible CoCrMo for orthopedic implants — if it pours, we've spec'd the line.
| Alloy | Specification | Sectors | Max Service Temp | Yield Strength |
|---|---|---|---|---|
| IN718 (Inconel 718) | AMS 5662 | AerospaceEnergy | 650°C | 1,034 MPa |
| René 80 | GE B50TF115 | AerospaceDefense | 950°C | 862 MPa |
| CoCrMo (ASTM F75) | ASTM F75 Grade A | MedicalOrthopedic | 1,220°C | 655 MPa |
| Ti-6Al-4V ELI | ASTM F136 | MedicalAerospace | 315°C | 827 MPa |
| 17-4 PH Stainless | AMS 5643 | DefenseIndustrial | 480°C | 1,170 MPa |
| Mar-M 247 | AMS 5757 | AerospaceEnergy | 1,000°C | 896 MPa |
Proven on
the Floor.
280+ lines commissioned across 18 countries. Every machine validated to the certification your customer requires — Nadcap, AS9100D, ISO 13485, ITAR. No exceptions.
“The FDY-SB shell dipping line cut our ceramic build cycle by 18% while holding tighter coat thickness variance than our previous system. Three shifts in, zero recalibration.”
“We validated the FDY-VP vacuum furnace against ASTM F75 spec for our CoCrMo hip stem program. First-article acceptance on cycle two. That doesn't happen with off-the-shelf equipment.”
“Foundry's engineering team understood our MIL-SPEC requirements before the first site visit. The knockout and finishing cell they configured runs our armor component program at 94% OEE.”
“The furnace is already glowing before anyone clocks in.”
Build Your
Line.
Tell us your casting type, annual volume, and the stage you need to upgrade. Our engineering team responds with a preliminary line configuration — no boilerplate, no sales pitch.
What Happens Next
Engineering reviews your configuration within 1 business day
Preliminary equipment spec and floor layout delivered
Site visit scheduled if configuration fits your program
Full Equipment Spec Sheet
38-page PDF: every machine in the FDY line with complete dimensional drawings, electrical requirements, compatible alloy tables, and Nadcap/AS9100D compliance documentation. Built for your capex committee.